
Short-cycle welding is used for stud diameters from 3 to 10 mm. Its particular advantage is that, thanks to the short, shallow penetration compared to the other drawn arc processes, thinner sheets can also be welded (1/8 x D). The welding time is 5 to 100 ms at a current of up to 1900 A.
It is characterised by its good suitability for automation and can also be combined with shielding gas welding.
The short-cycle process works as follows:
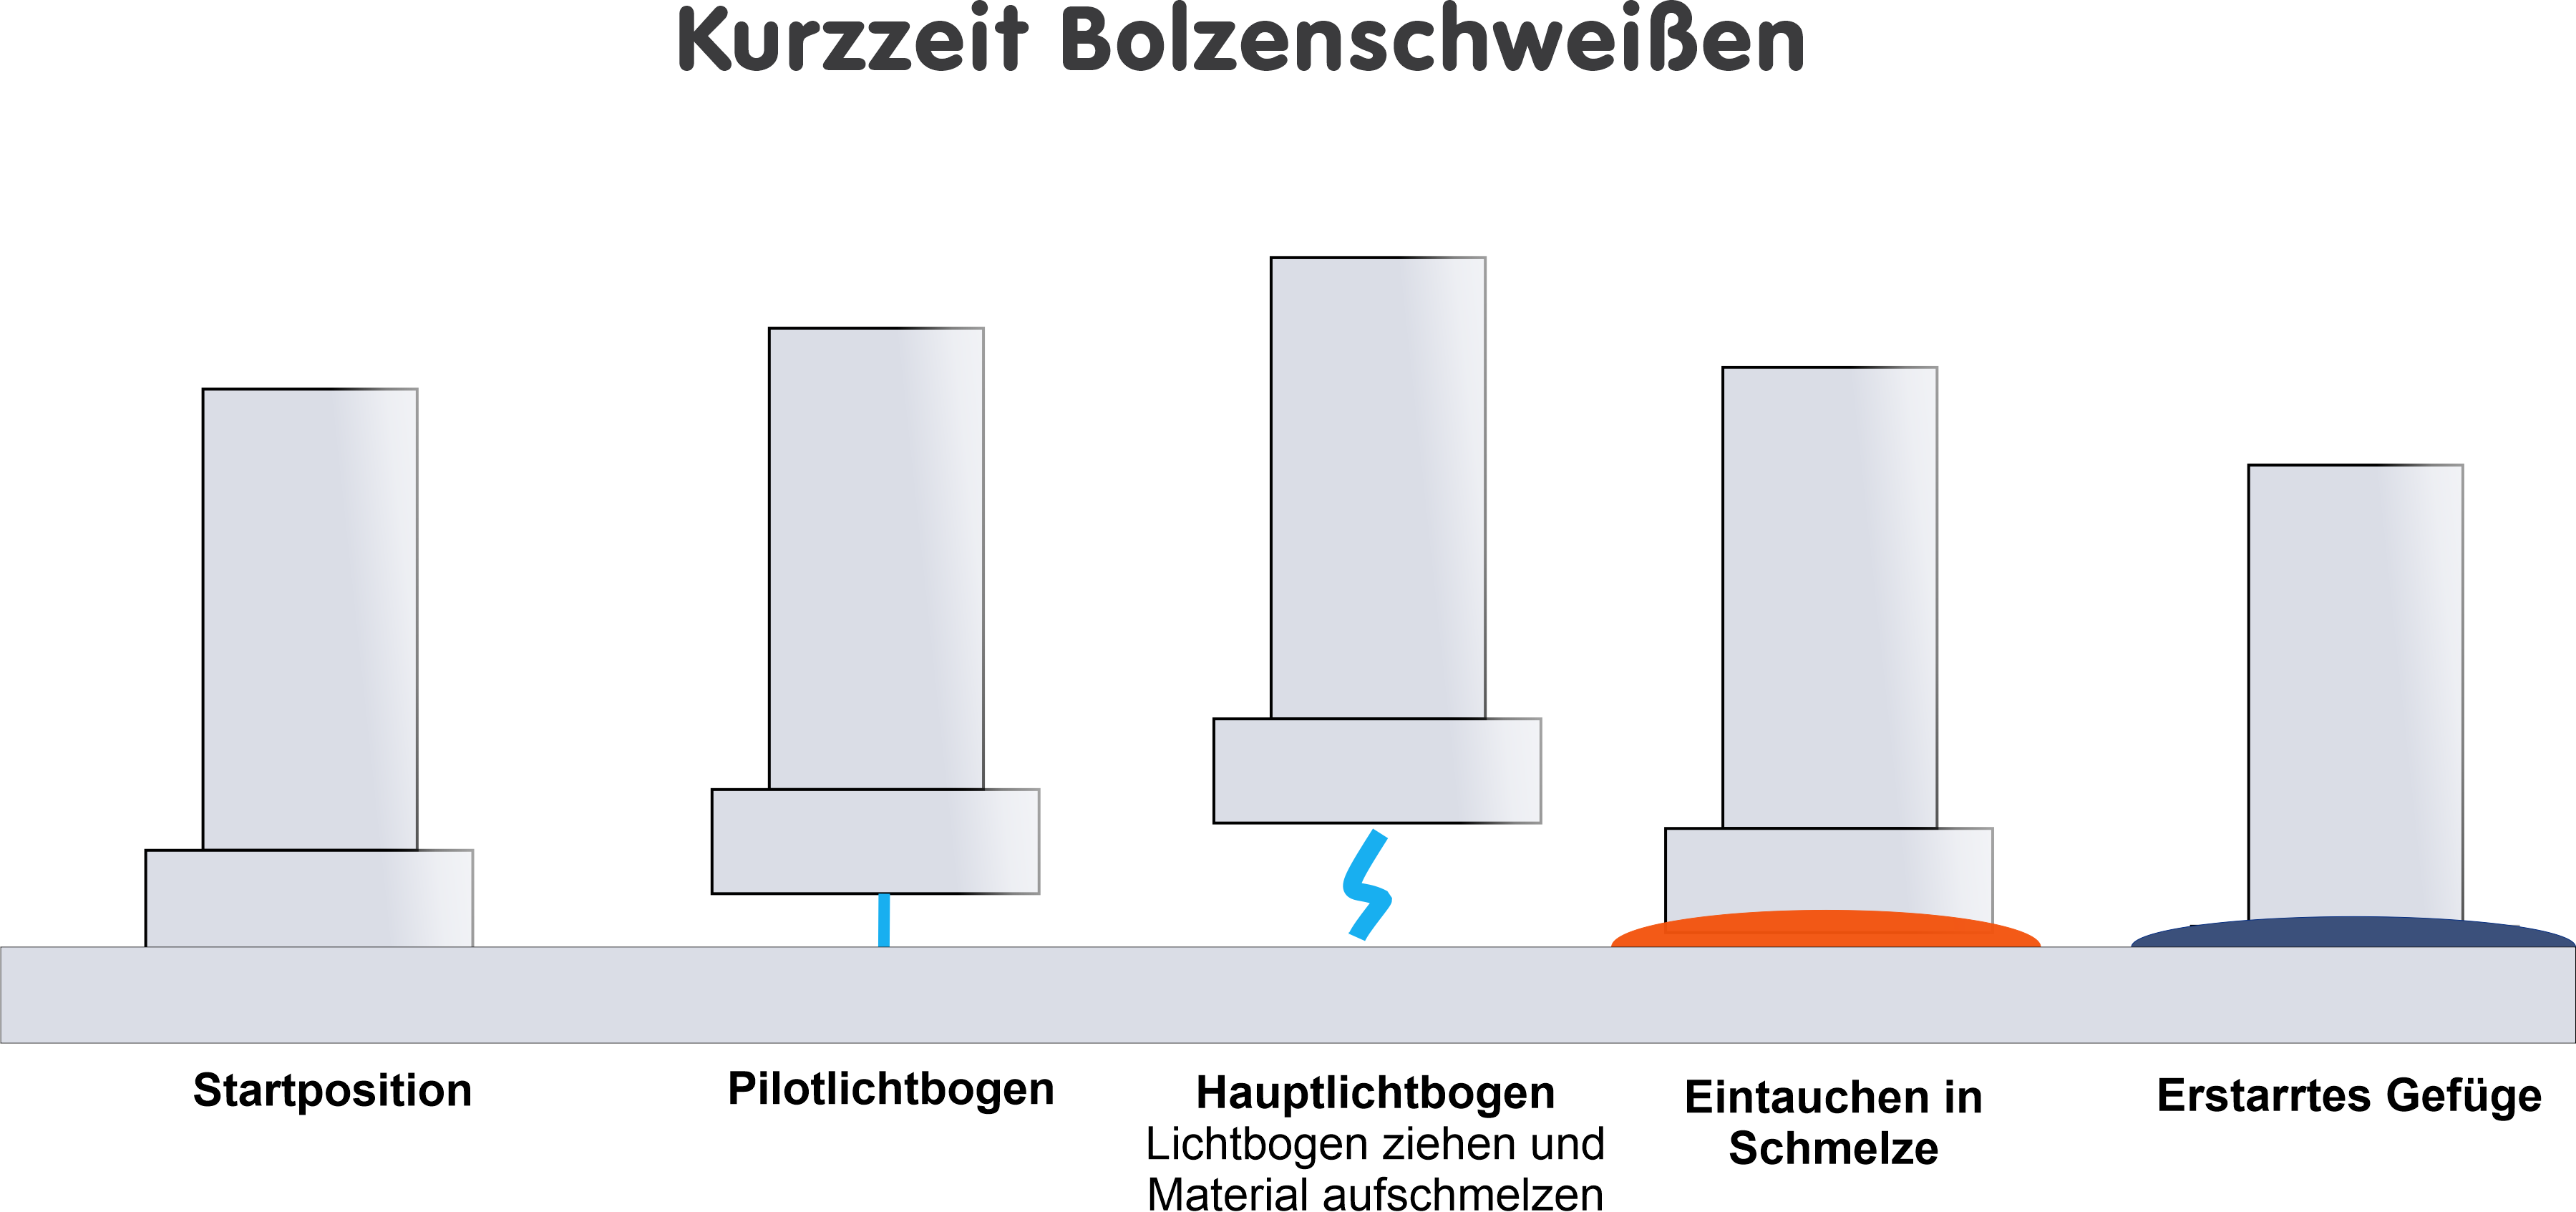
At the start, the stud sits on the workpiece and is lifted off it. A pilot arc is first generated with a low current. After a short "holding time", the main arc, which actually melts the materials, is ignited.
Throughout the welding process, the stud is thus lifted off the workpiece within the set welding time, which is considerably shorter in short-cycle welding than in ceramic ferrule welding, and then plunged back into the molten pool of the workpiece. This joins the stud to the workpiece.
The result is a firmly welded stud. The graphic shown here illustrates the welding process schematically.