
2.3 Aluminium Ball and Other Fluxes
2.7 Tightening Torques for Threaded Studs
2.8 Strength of Weld Stud Connections
Technical Information
2.1 Materials
Materials according to DIN EN ISO 13918 are used for all common stud types. Special materials are possible on request; we will be happy to check their availability and weldability for you and advise you on your welding task.
When placing your order, please let us know whether you require a test report 2.2 or an inspection certificate 3.1 according to DIN EN 10204.
1. Unalloyed steel, property class 4.8 (comparable to former St37)
ARNHOLD weld studs are made of steel of property class 4.8 (DIN EN ISO 898-1) with excellent welding properties.
Re ≥ 340 N/mm², Rm ≥ 420 N/mm², elongation A5 ≥ 15 %
2. Stainless steel (A2-50)
Stainless steel weld studs are usually made of A2-50 (DIN EN ISO 3506-1).
Rp0.2 ≥ 210 N/mm², Rm ≥ 500 N/mm², elongation after fracture A ≥ 0.6d
The materials A4 (1.4401), A5 (1.4571) and 16Mo3 (1.5415) are also used.
2.2 Dimensions
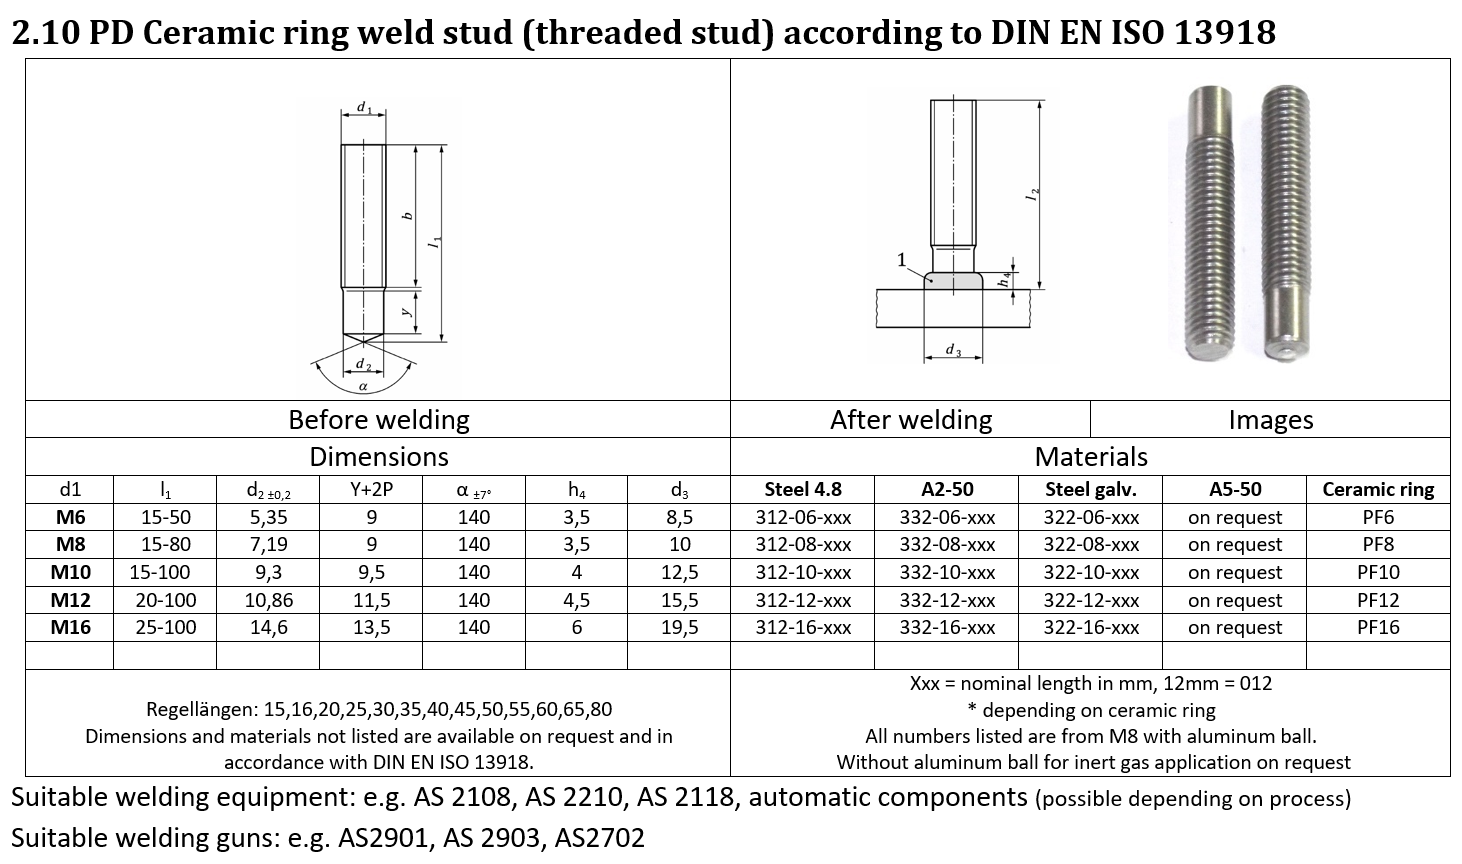
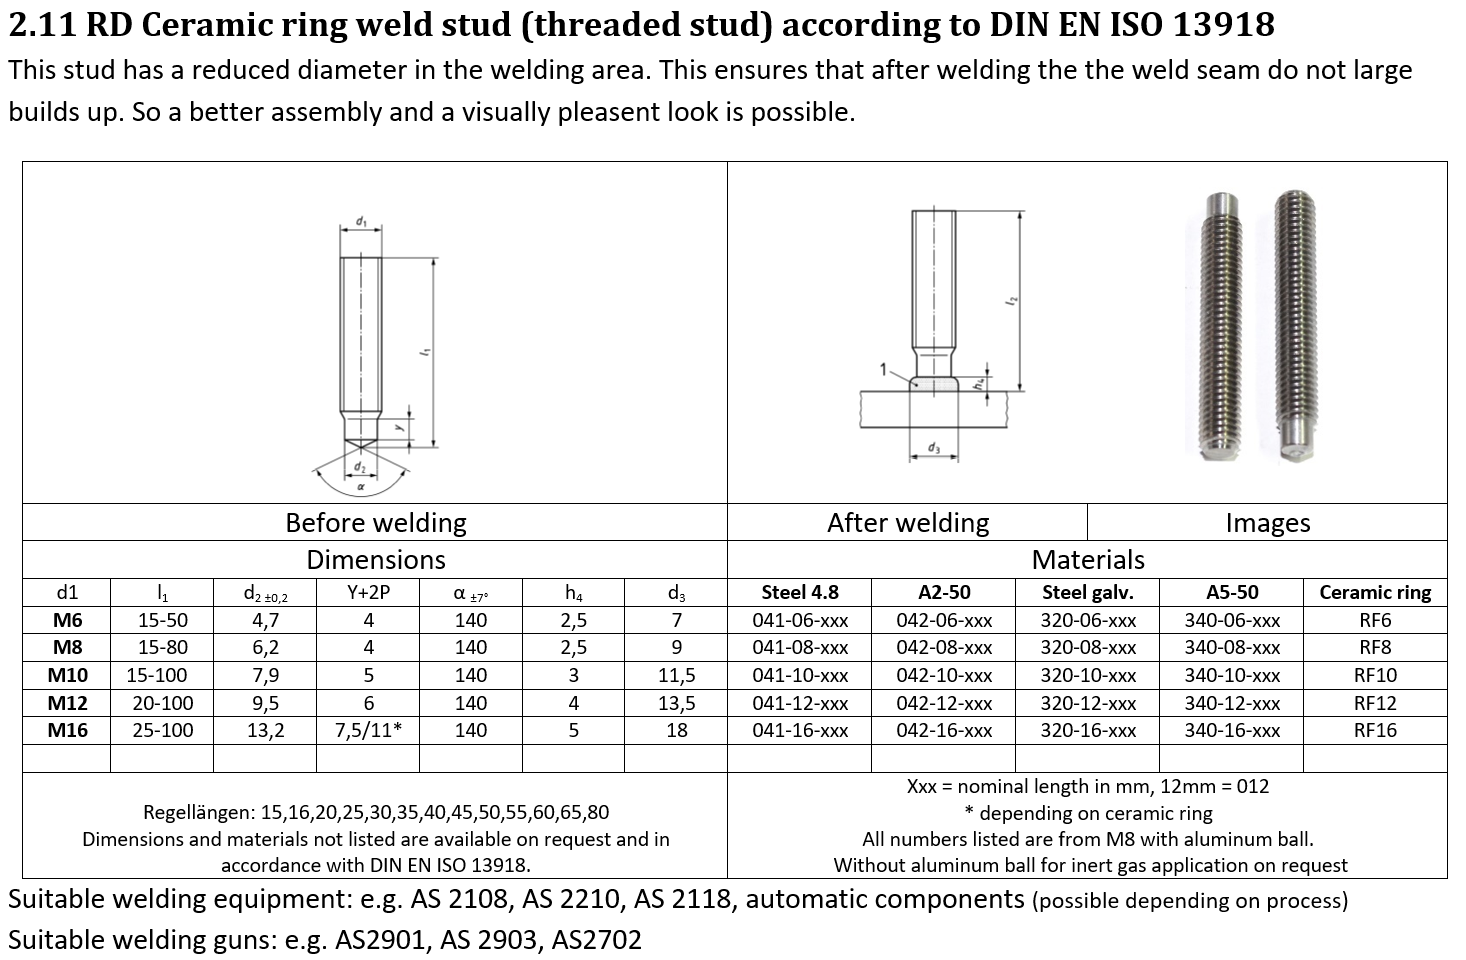
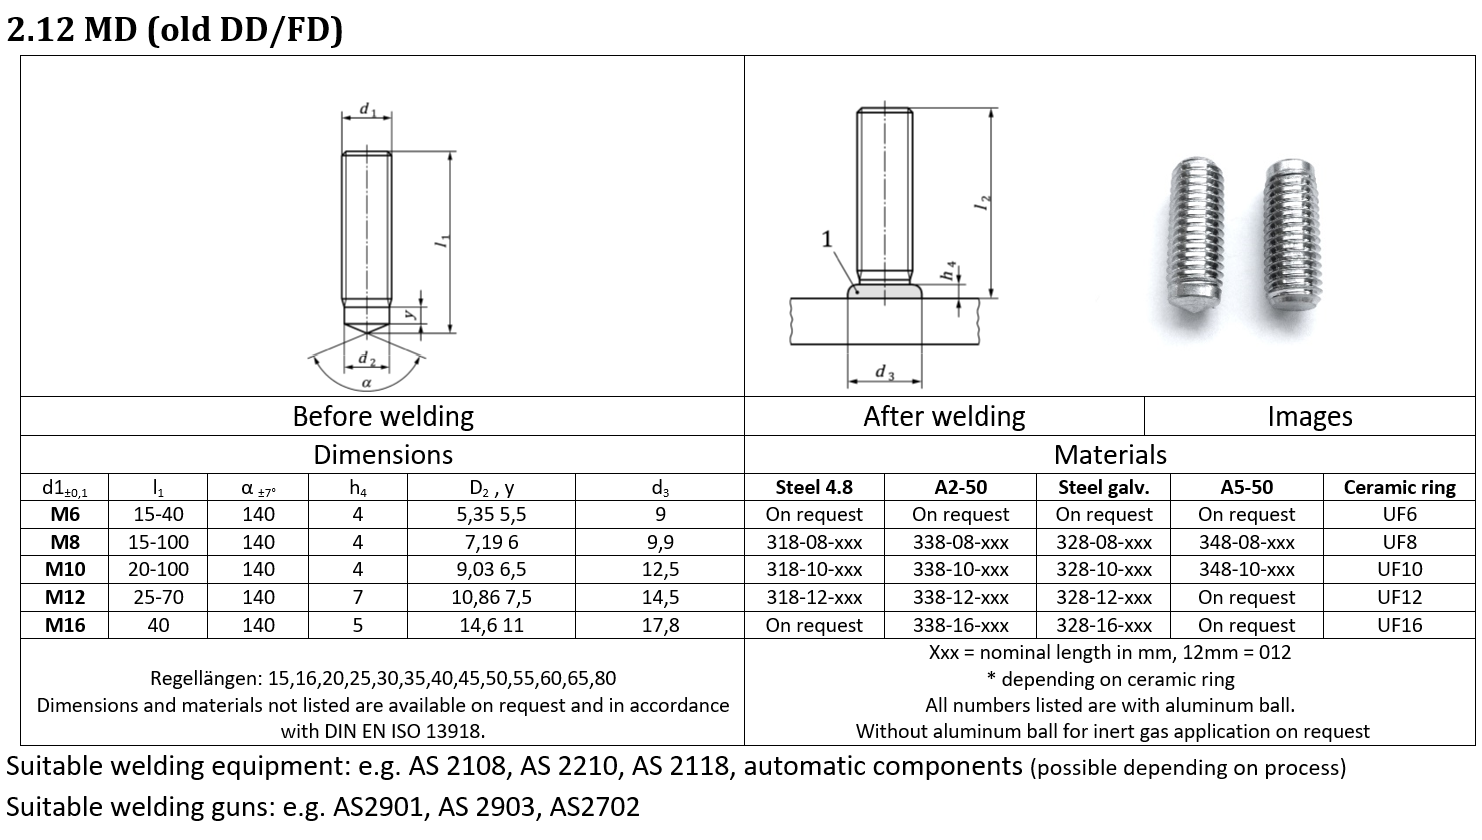
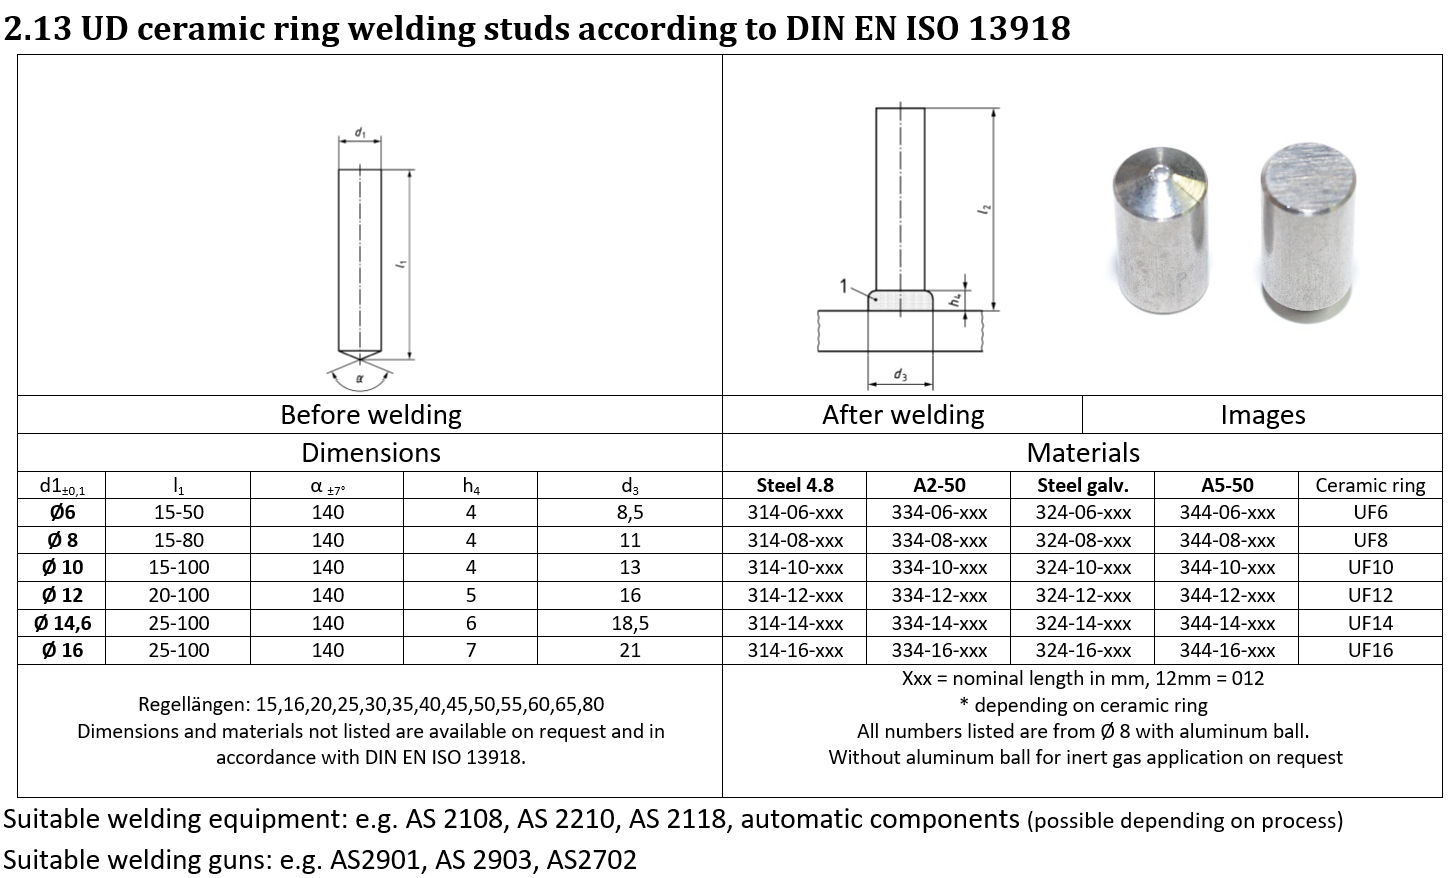
Please refer to the corresponding tables for the dimensions of your stud type. Standard studs are manufactured according to DIN EN ISO 13918. Dimensions not listed and special shapes are also based on this standard to ensure the best welding results.
Drawn arc studs are shortened during welding (burn-off). The specified article lengths always refer to the nominal stud length after welding.
The length allowance of 1 to 5 mm is dimensioned so that the stud reaches its nominal length when the recommended welding parameters are used.
2.3 Aluminium Ball and Other Fluxes
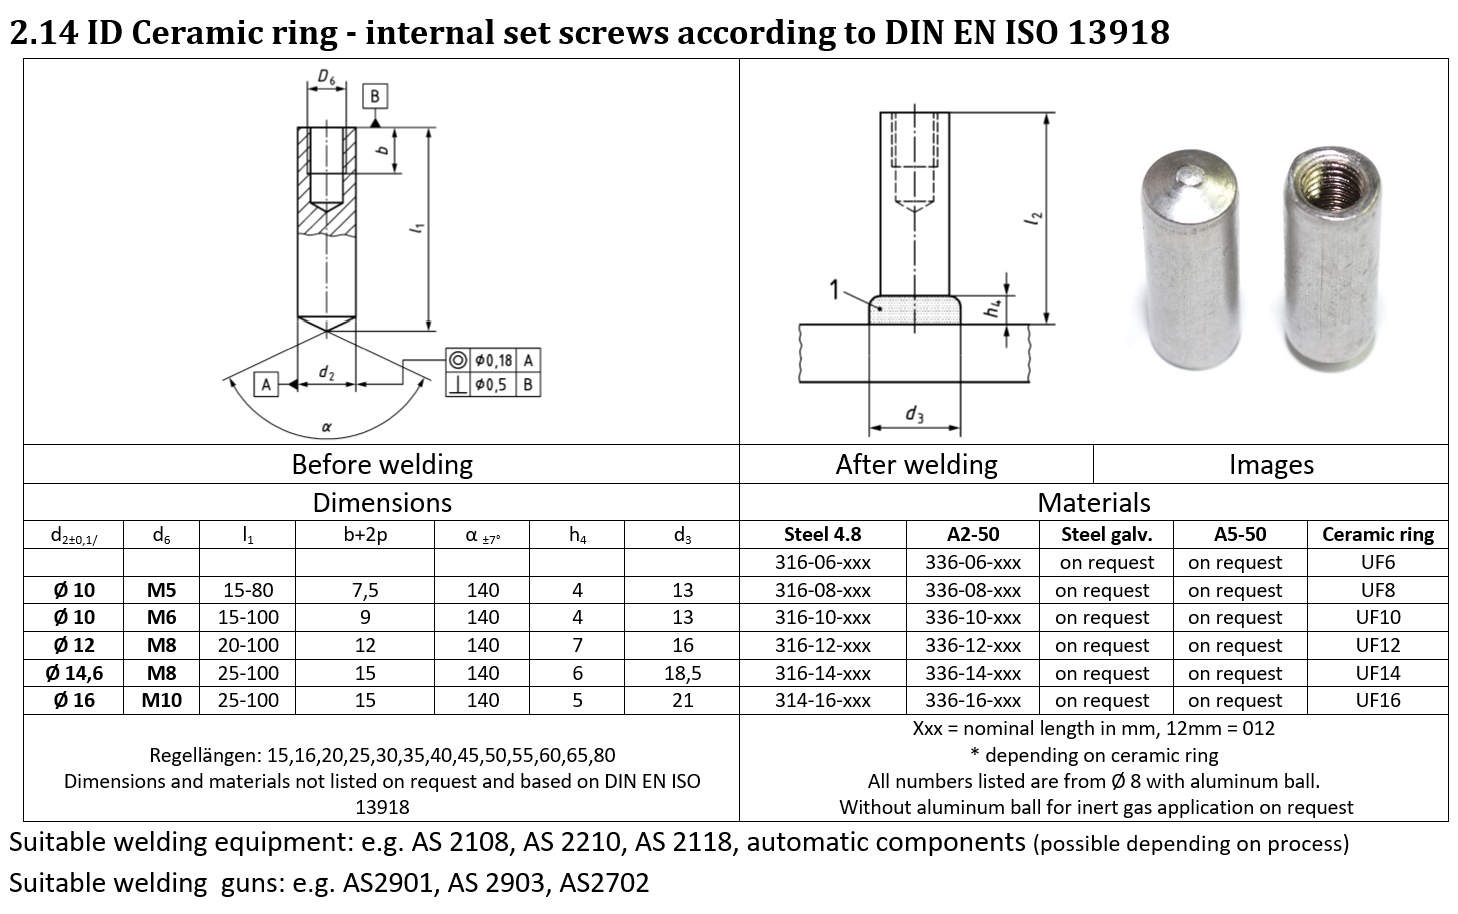
Weld studs with diameters from 6 to 16 mm for welding with ceramic ferrules are provided with aluminium in the weld area, usually in the form of a pressed-in aluminium ball.
Studs up to M10 can also be welded under shielding gas without a ceramic ferrule. In this case, studs without an aluminium ball should be used to avoid weld defects and to improve the flow properties of the weld pool. Increased arc blow must be expected under shielding gas, and welding in positions other than flat is more difficult.
2.4 Ceramic Ferrules
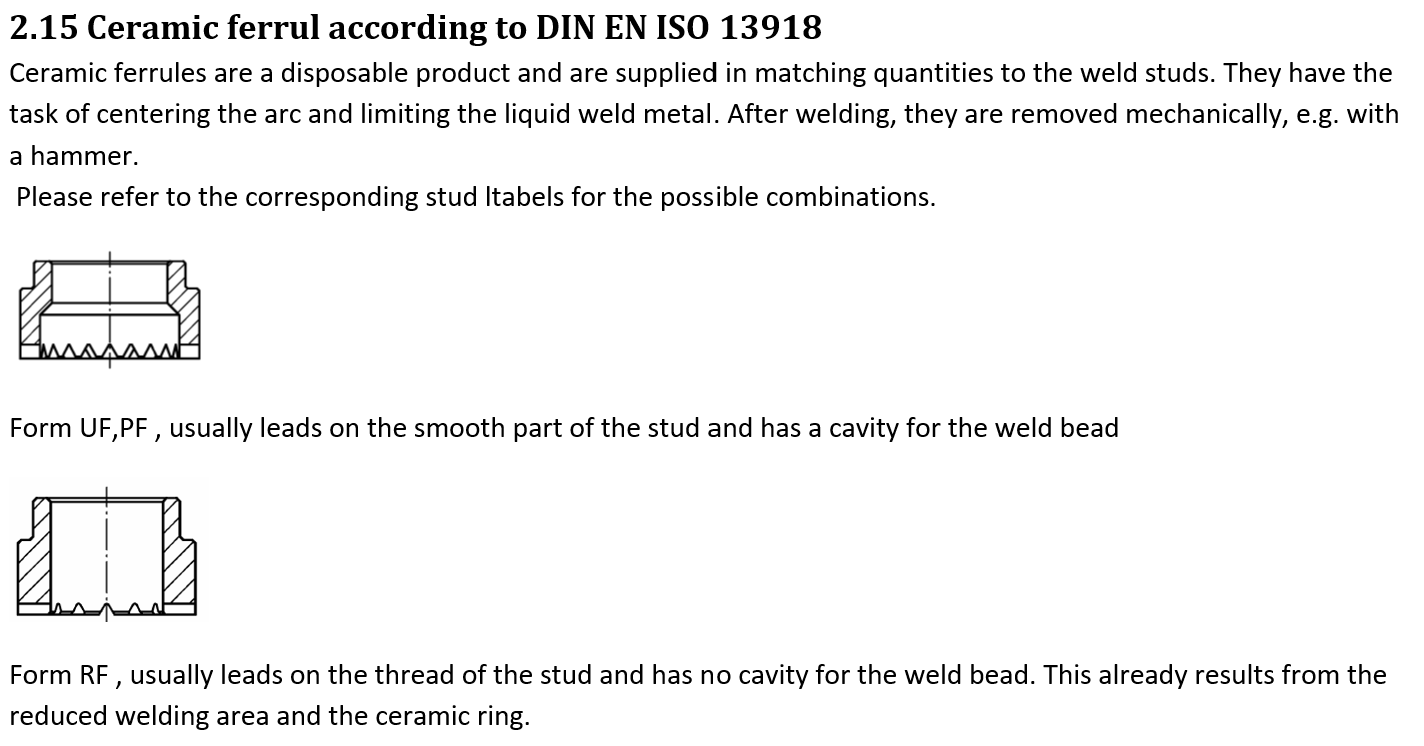
Each stud for ceramic ferrule welding requires a ceramic ferrule, which shields and shapes the weld pool. The ferrules are supplied in matching quantities with the studs and can only be used once; they are broken off after welding.
Ceramic ferrules must be stored in a dry place to achieve the best welding results. Re-drying ferrules that have become damp is generally neither economical nor effective.
2.5 Surface Finishes
Drawn arc studs are usually supplied uncoated (bright).
The following surface finishes are available on request:
- Electroplated zinc
- Electroplated zinc, yellow chromated (not RoHS compliant)
- Electroplated zinc, blue passivated (RoHS compliant)
- Zinc flake coating
- Electroplated copper and nickel
- Electroplated copper
For finishes 1 to 4, the coating is mechanically removed from the weld area after coating to improve weldability.
2.6 Threads
Threads are usually cold rolled and comply with tolerance class 6g for uncoated studs and 6h for coated studs.
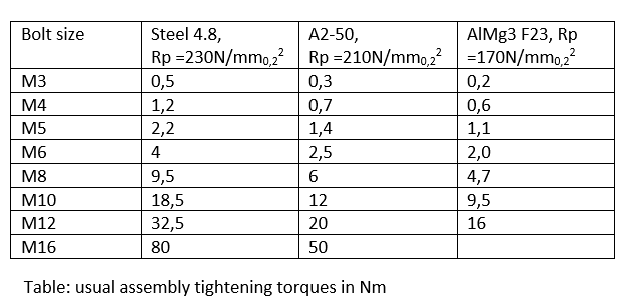
2.7 Tightening Torques for Threaded Studs
The following table provides guideline values for the minimum tensile force and the tightening torque of a welded connection without permanent deformation of the joined components. A sufficient wall thickness of the components is required.
The values apply to threaded studs with standard metric threads, without surface coating and without thread lubrication. The tensile stress area must be present over the entire stud length (not applicable to RD studs). The values are based on the specified yield strengths.
These values are non-binding guideline values for the stated conditions and must be adapted to the actual application.
2.8 Strength of Weld Stud Connections
As a general rule, if welding is carried out correctly, the connection will not fail in the weld area. Deformation or fracture therefore normally occurs in the stud or in the base material.
Exceptions may occur with weld studs featuring a reduced weld area (e.g. mini flange studs) or with unsuitable material combinations, such as joints between carbon steel and stainless steel. These cases must be assessed separately. If in doubt, the quality of these connections must be verified by means of a welding procedure test.
The load limit used for calculations is determined by the properties of the base material or the stud material and by the applied forces. The decisive factor for strength calculations is the stress in the tensile stress area together with the relevant material properties, taking into account an appropriate safety factor.