
1.7 Tightening Torques for Threaded Studs
1.8 Strength of Weld Stud Connections
Technical Information
ARNHOLD weld studs are manufactured on modern machines using the cold heading process to ensure the highest product quality. All weld studs are subject to continuous quality control to guarantee optimum welding results.
1.1 Materials
Unless otherwise specified, the materials comply with DIN EN ISO 13918 "Studs and ceramic ferrules for arc stud welding".
- Steel
Property class 4.8 (weldable) according to ISO 898-1, comparable to S235
Re ≥ 340 N/mm² - Stainless steel A2-50
DIN EN ISO 3506-1
Rm ≥ 500 N/mm², Re ≥ 210 N/mm² - Stainless steel A5-50
DIN EN ISO 3506-1 - Aluminium AlMg3
Rm ≥ 100 N/mm² - Brass CuZn37
Rm ≥ 370 N/mm² - Other materials on request
1.2 Dimensions
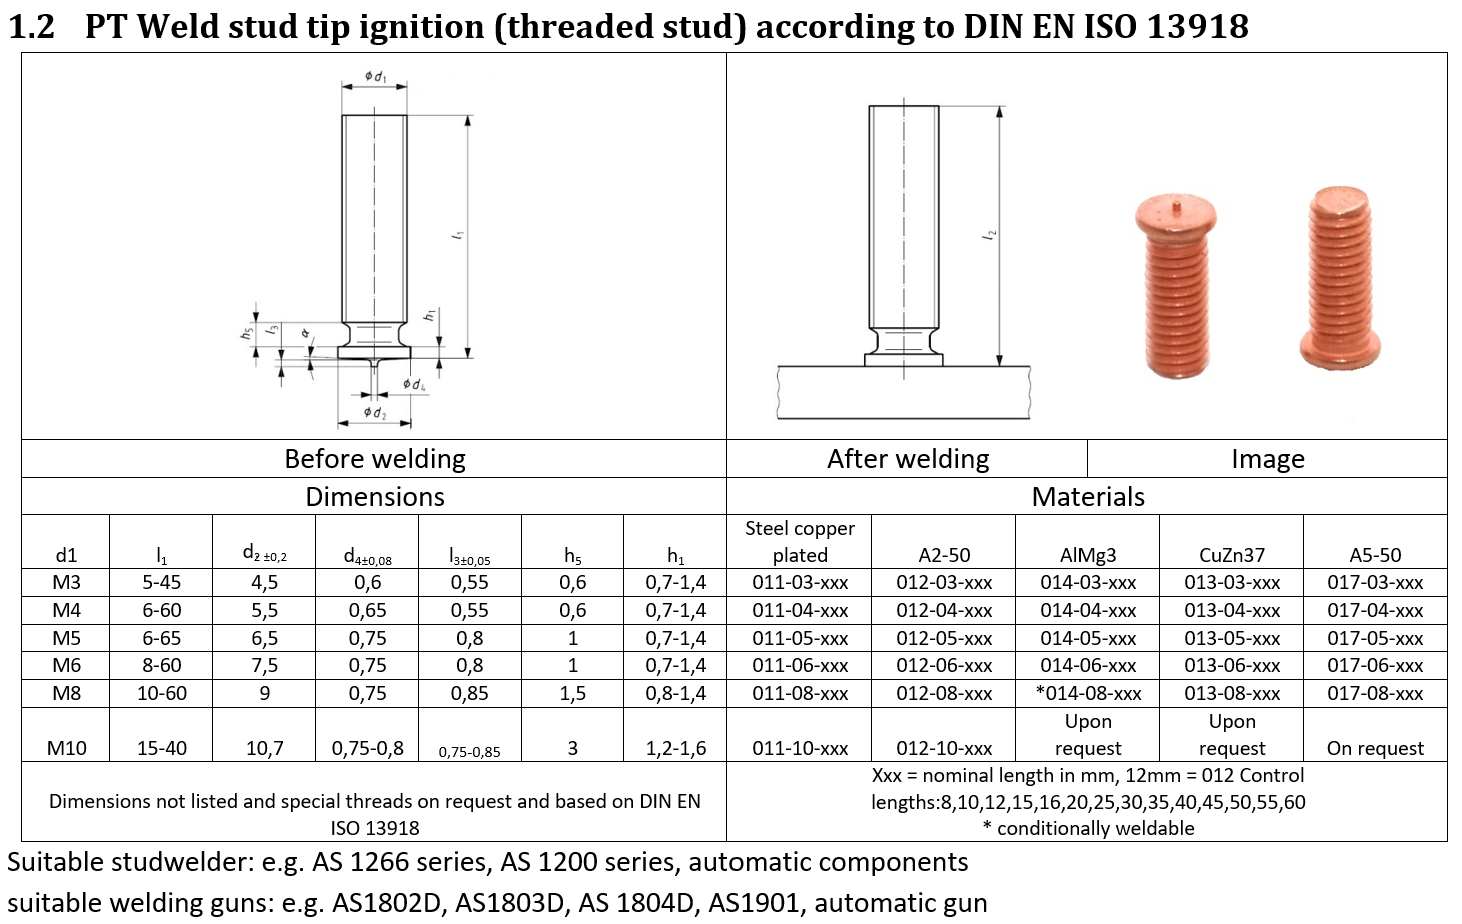
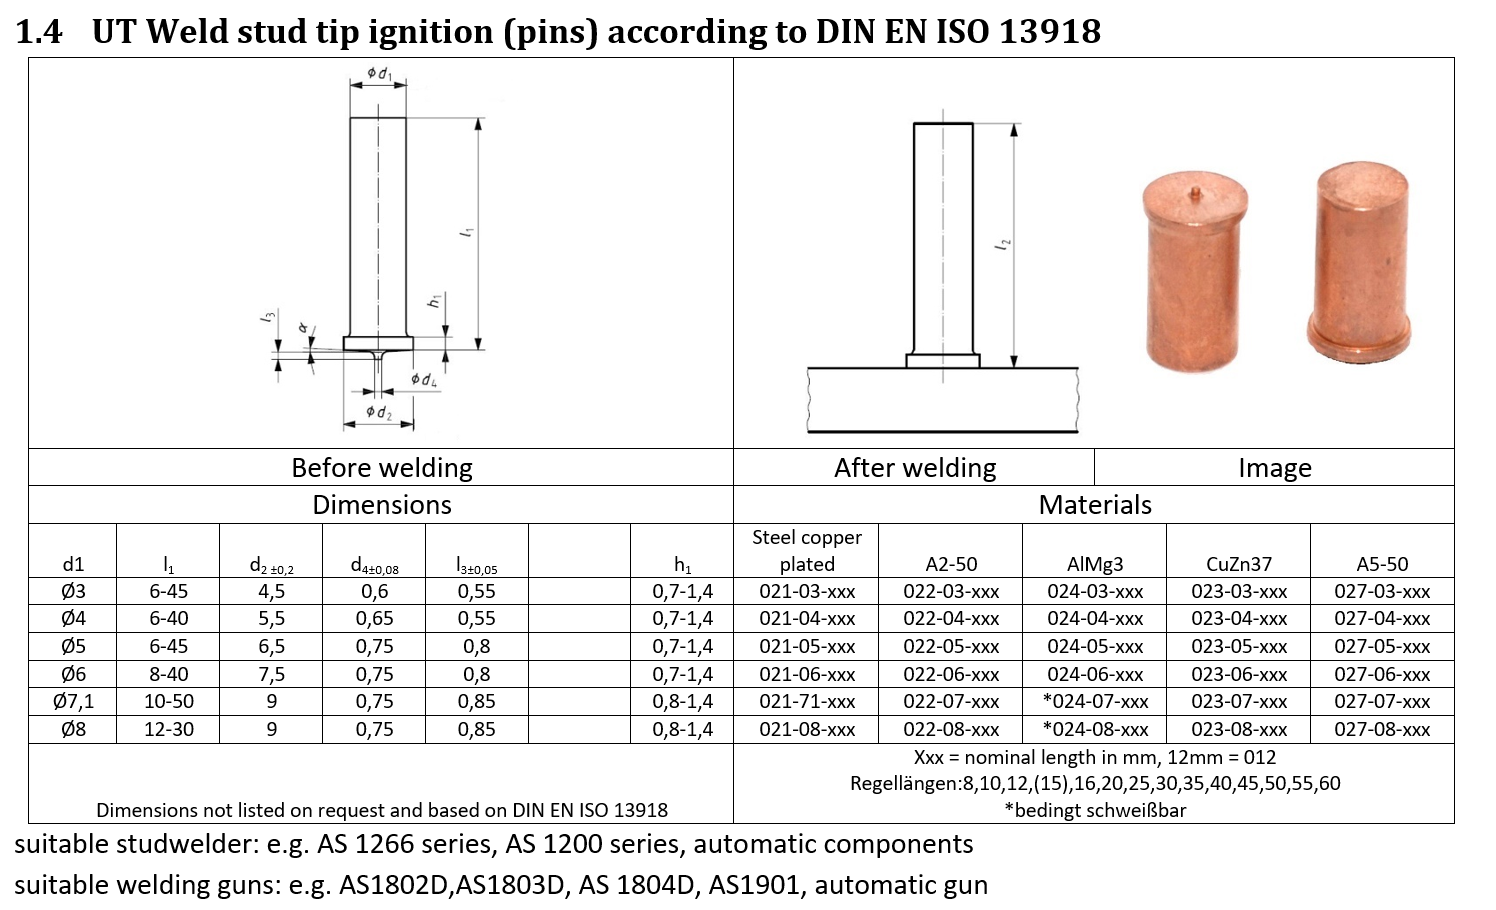
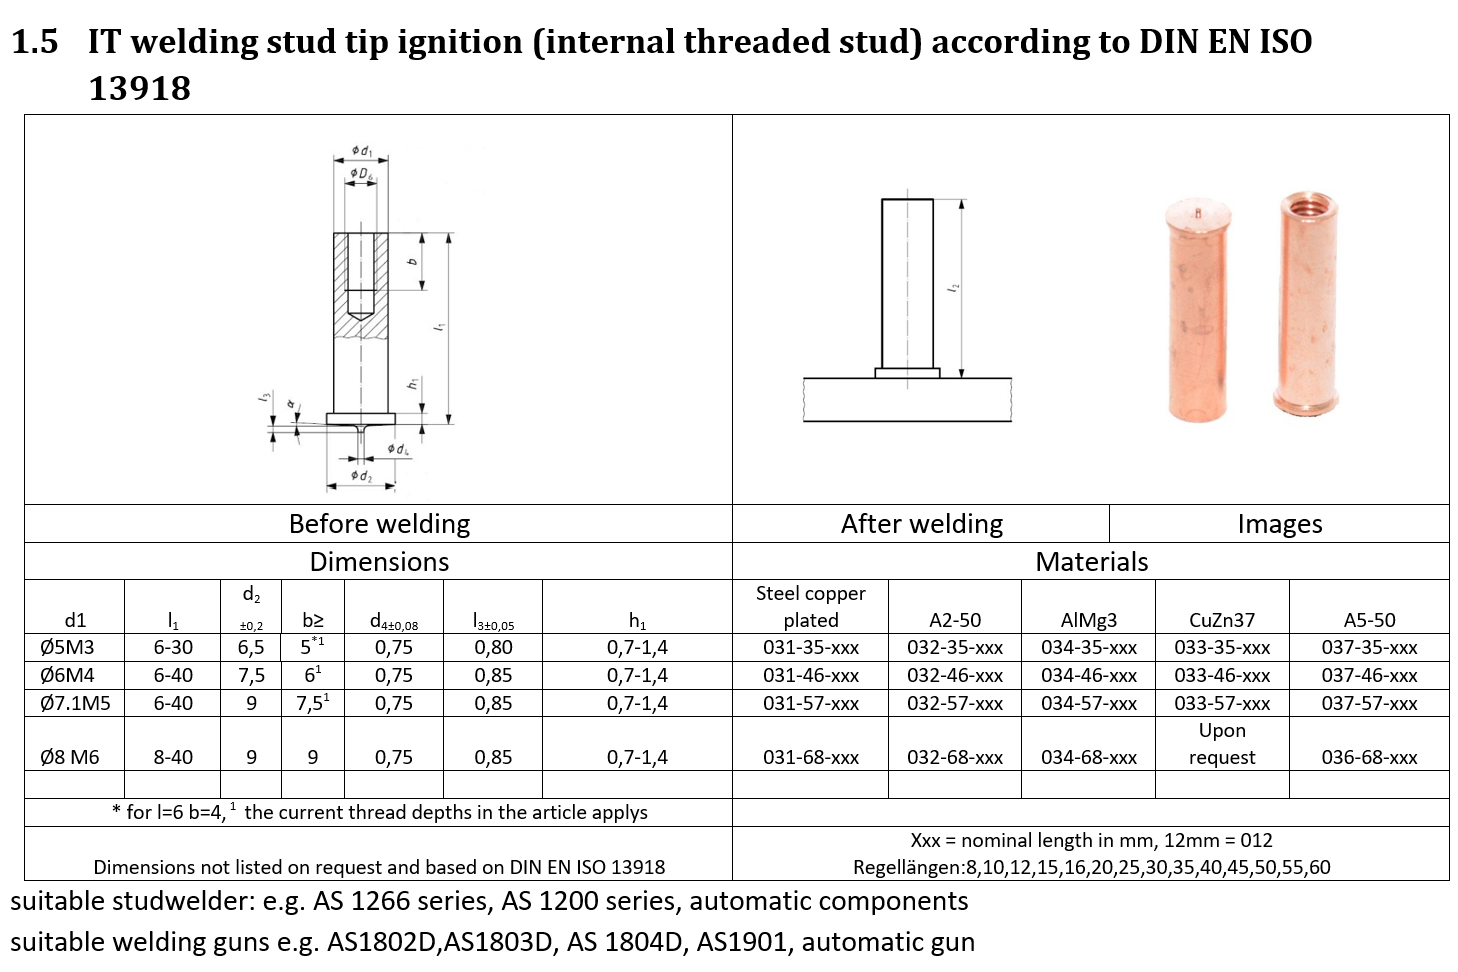
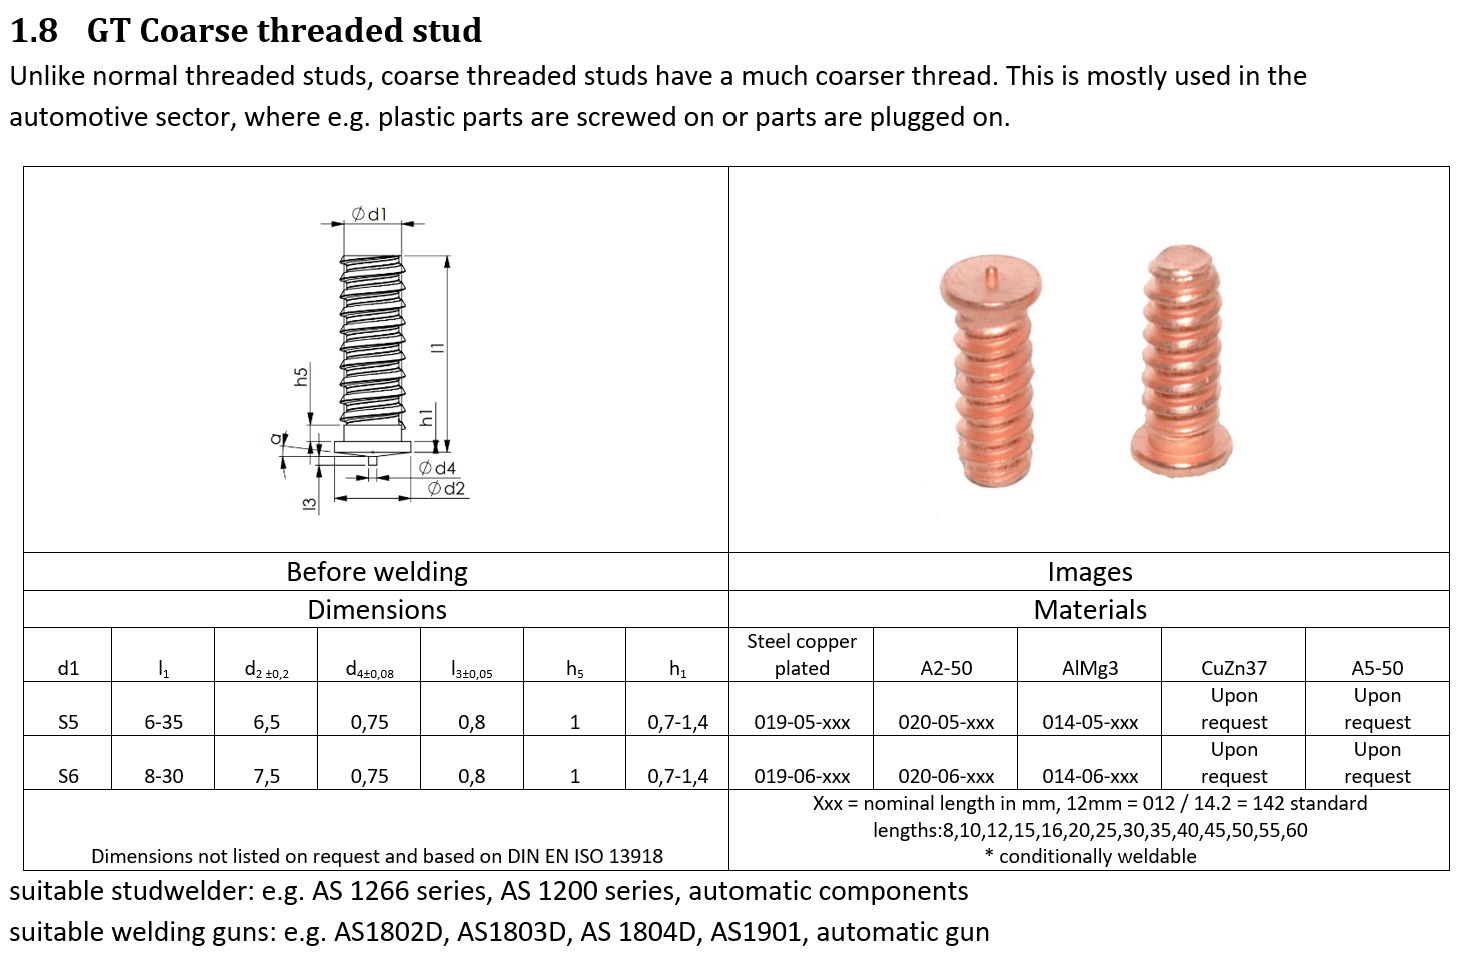
The dimensions [in mm] of the studs are specified in the respective tables. All standard weld studs comply with DIN EN ISO 13918:2008. Non-standard studs are manufactured based on this standard. Special parts according to customer drawings are available on request.
External threads are generally cold rolled and comply with tolerance class 6g. The resulting work hardening provides excellent tensile and pull-out strength in the threaded area.
1.3 Surface Finish (DIN EN ISO 13918:2008)
Steel studs are usually copper-plated. Unless otherwise specified, the coating corresponds to C1E (4 to 8 µm).
Zinc plating, tin plating, nickel plating and other surface finishes are available on request.
1.4 Stud Flange
The stud flange increases the weld area and provides favourable conditions for arc ignition. It also ensures reliable feeding. A certain out-of-roundness of the flange within the specified tolerances is process-related and normal.
For special applications with lower strength requirements, studs with mini flanges are also available. Please contact us for further information.
1.5 Ignition Tip
A precisely formed ignition tip is essential for a reliable welding process, which is why the tolerances are very tight. For optimum welding results, each delivery batch should nevertheless be processed separately.
1.6 Use
Unless otherwise specified, the weld studs are supplied for manual feeding.
Optically sorted products for the highest quality requirements are available on request.
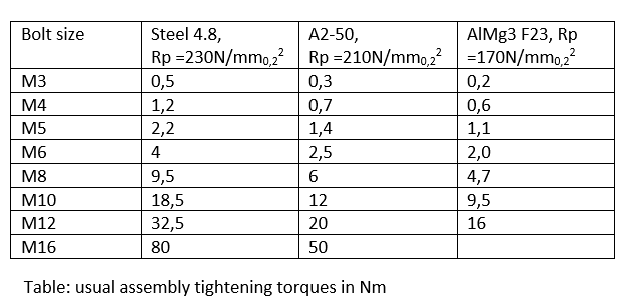
1.7 Tightening Torques for Threaded Studs
The following table provides guideline values for the minimum tensile force and the tightening torque of a welded connection without permanent deformation of the joined components. A sufficient wall thickness of the components is required.
The values apply to threaded studs with standard metric threads, without surface coating and without thread lubrication. The tensile stress area must be present over the entire stud length (not applicable to RD studs).
The values are based on the specified yield strengths.
These values are non-binding guideline values for the stated conditions and must be adapted to the actual application.
1.8 Strength of Weld Stud Connections
As a general rule, if welding is carried out correctly, the connection will not fail in the weld area. Deformation or fracture therefore normally occurs in the stud or in the base material.
Exceptions may occur with weld studs featuring a reduced weld area (e.g. mini flange studs) or with unsuitable material combinations, such as dissimilar metal joints. These cases must be assessed separately.
If in doubt, the quality of these connections must be verified by means of a welding procedure test.
The load limit used for calculations is determined by the properties of the base material or the stud material and by the applied forces. The decisive factor for strength calculations is the stress in the tensile stress area together with the relevant material properties, taking into account an appropriate safety factor.